 English
A printed circuit board assembly can pass a basic power-on test and still fail after installation, shipment, vibration, thermal cycling, or months of field use. For OEMs, effective PCBA quality control means preventing defects at each manufacturing stage, detecting the faults that escape prevention, and proving that the finished assembly meets documented acceptance criteria. The goal is not simply to produce a board that works once. It is to deliver repeatable performance across prototypes, pilot builds, and volume production.
Quick Answer: What Matters Most in PCBA Quality Control?
PCBA quality control is the combination of process controls, inspections, electrical tests, traceability, and corrective actions used to verify that a populated circuit board conforms to its design and reliability requirements.
Before assembly: Validate the BOM, approved components, PCB fabrication data, solder-paste requirements, and revision control.
During assembly: Monitor solder-paste printing, component placement, reflow profiles, handling, and workmanship.
After assembly: Use appropriate AOI, X-ray inspection, in-circuit testing, and functional testing based on board complexity and risk.
For production release: Require documented acceptance criteria, traceability, nonconformance control, and corrective-action records.
For OEM sourcing: Compare suppliers by demonstrated process capability and defect-prevention systems, not by unit price or promised turnaround alone.
Our recommendation: Agree on the quality plan before placing the production order. Adding inspection after defects have already been built into a batch is usually more expensive than preventing those defects upstream.
1. What Is PCBA Quality Control?
PCBA quality control is the planned verification of a printed circuit board assembly throughout manufacturing. It covers incoming materials, component identity, soldering, placement accuracy, electrical performance, workmanship, and the records needed to demonstrate conformity. It is broader than a final visual inspection and more practical than relying on a supplier's general statement that every board is tested.
Quality control and quality assurance are related but different. Quality assurance establishes the systems and procedures intended to prevent defects. Quality control checks whether materials, processes, and finished assemblies meet specified requirements. An OEM needs both: a supplier may inspect thoroughly yet continue producing the same defect if the underlying process is not corrected.
The exact control plan depends on the product. A simple controller with accessible test points does not need the same inspection strategy as a dense board containing fine-pitch packages, hidden solder joints, high-speed interfaces, or safety-related circuitry. For boards using specialized constructions such as an electronic load board PCB, an IC substrate PCB, or a SiP PCB, inspection planning must reflect the assembly's actual geometry and intended function.
Practical distinction: “100% inspected” does not automatically mean “100% defect-free.” An inspection system can only detect the failure modes it is designed and configured to detect. OEMs should ask what is inspected, how acceptance is defined, what is recorded, and how failures are handled.
2. How the PCBA Quality Control Process Works
A reliable control plan follows the product from engineering release to shipment. The strongest process links every checkpoint to a known risk and a documented response when results fall outside the acceptance criteria.
Step 1: Review design and manufacturing readiness
Before production, verify that the assembly drawing, Gerber or equivalent fabrication data, bill of materials (BOM), pick-and-place file, approved substitutions, polarity markings, and firmware or test requirements all refer to the correct revision. Confirm component package sizes, footprint compatibility, thermal constraints, and any special soldering requirements.
For prototypes, a design-for-manufacturing review can uncover pad, spacing, orientation, or test-access problems before they become recurring production defects. If a design uses a flexible PCB or rigid-flex PCB, the review should also consider bend areas, stiffeners, connector strain, and handling limits.
Step 2: Verify incoming materials
Incoming control should confirm part numbers, manufacturer identity where required, quantities, lot information, packaging condition, and storage requirements. Moisture-sensitive components may need controlled storage and handling under the applicable component instructions. Solder paste, adhesives, and other process materials also need valid shelf life and appropriate storage conditions.
Do not treat a supplier label as complete proof of authenticity. For high-risk components, OEMs may require approved-source controls, additional documentation, or risk-based verification. Any substitution should be formally approved before assembly, not silently introduced to protect a delivery date.
Step 3: Control solder-paste printing and component placement
Insufficient, excessive, shifted, or bridged solder paste can create open joints, shorts, solder balls, and inconsistent solder fillets. Solder-paste inspection can help verify deposit volume, area, height, and alignment when the process and board risk justify it. Placement machines should be set up against the correct program, component orientation, feeder data, and board revision.
Step 4: Verify the reflow or soldering process
Reflow profiles must suit the solder paste, component mix, PCB thermal mass, and manufacturer recommendations. Excessive heat can damage components or laminate; insufficient heat can result in poor wetting or incomplete joints. A profile should be measured and validated rather than assumed correct because the oven uses a familiar recipe.
Through-hole and mixed-technology assemblies may require wave soldering, selective soldering, or controlled hand soldering. Each process needs suitable acceptance criteria and operator controls. The appropriate method depends on board design and component requirements, not simply the lowest process cost.
Step 5: Inspect, test, and record results
Automated optical inspection (AOI) can detect many visible placement and soldering defects. X-ray inspection helps assess hidden joints where the package design makes optical inspection insufficient. In-circuit testing (ICT) checks electrical nodes and components where test access and fixture economics allow it. Functional testing evaluates whether the assembly performs its specified functions under defined conditions.
Step 6: Control nonconformities and release the batch
Defects should be logged, contained, evaluated, and dispositioned through an agreed process. Depending on the issue, the response may be rework, repair, scrap, or a formally approved concession. Repaired boards should be re-inspected or re-tested as appropriate. The supplier should retain records that connect the released batch to its relevant inspection and test results.
3. Eight Critical Quality-Control Checkpoints
1. BOM and revision control
A technically sound board can fail because the assembly line used an obsolete BOM, incorrect component value, or unapproved substitute. Establish a single released document set and a clear engineering-change procedure. For recurring orders, confirm that the supplier's work instructions and machine programs have been updated after every approved change.
2. Component authenticity and lot traceability
Counterfeit, misidentified, damaged, or poorly stored components can create failures that are difficult to diagnose after shipment. Traceability is especially important for long-life products, regulated markets, and assemblies with costly field replacement. Define the level of traceability required: component lot, date code, supplier lot, assembly batch, serial number, or a combination.
3. Solder-paste deposit quality
Solder-paste printing is an early source of assembly defects. Inspect stencil condition, alignment, paste handling, board support, and printing parameters. SPI is useful when fine-pitch parts, small passives, or high-density assemblies make deposit variation a meaningful risk. It is not a substitute for proper stencil design and process setup.
4. Component placement and polarity
Incorrect orientation, missing parts, shifted components, and wrong package variants can all create functional failures. AOI programs should be validated against the released design and should account for legitimate visual differences, such as reflective finishes or component markings. False calls need attention too: if operators repeatedly override alarms, the inspection system becomes less effective.
5. Solder-joint integrity
Cracked joints, insufficient wetting, bridges, voiding, and lifted leads have different causes and consequences. Acceptance should follow an agreed workmanship standard, such as the relevant class and criteria of IPC-A-610, where contractually applicable. Do not assume that every void, mark, or cosmetic irregularity is automatically a failure; assess it against the applicable standard, package requirements, and product risk.
6. Hidden-joint inspection
Ball-grid arrays and other packages with hidden terminations may require X-ray inspection. The method can reveal certain bridging, ball alignment, and void-related conditions, but interpretation depends on package design, image quality, and acceptance criteria. X-ray does not prove every joint is electrically sound, so it should be combined with other controls where necessary.
7. Electrical and functional verification
Testing should be designed around the product's failure modes. ICT may detect shorts, opens, and component-value issues when access and fixture coverage permit. Functional testing verifies behavior under defined operating conditions, but it may not expose every latent reliability problem. A simple power-on check is therefore insufficient for complex products unless the risk analysis shows that it covers the required acceptance criteria.
8. Documentation and corrective action
Inspection without useful records limits the OEM's ability to investigate failures and compare suppliers. Ask for defect summaries, test results, rework records, lot identification, and documented corrective actions appropriate to the project. When a defect repeats, the supplier should investigate the cause and verify whether the corrective action actually prevents recurrence.
| Checkpoint | Typical Risk | Useful Evidence | OEM Decision |
|---|---|---|---|
| Document control | Wrong revision or unauthorized substitution | Released BOM, revision history, approved change records | Do not release production until the document set is aligned. |
| Incoming materials | Wrong, damaged, or suspect components | Receiving records, lot data, approved-source records | Increase verification for high-risk parts. |
| Printing and placement | Bridges, opens, misalignment, wrong orientation | SPI/AOI results and process setup records | Prioritize controls for fine-pitch and dense assemblies. |
| Soldering | Poor wetting, thermal damage, inconsistent joints | Validated profiles and workmanship inspection | Require process validation for the actual board and materials. |
| Electrical testing | Shorts, opens, incorrect values, functional failure | ICT and functional-test records | Match coverage to product risk and test access. |
| Release and traceability | Uncontrolled rework or difficult failure analysis | Batch records, nonconformance reports, release approval | Define what evidence must accompany shipment. |
4. PCBA Inspection and Testing Methods Compared
No single inspection method catches every defect. The practical choice is a layered plan: use each method for the failure modes it can detect, and close the gaps with other inspections, tests, and process controls.
| Method | Best Use | Strength | Limitation | When to Choose It |
|---|---|---|---|---|
| Visual inspection | Obvious assembly and workmanship issues | Flexible and relatively inexpensive | Operator-dependent; limited access to small or hidden features | As a baseline, especially for prototypes and rework. |
| SPI | Solder-paste deposit verification | Finds printing variation before reflow | Does not verify final solder joints or board function | For fine-pitch, high-density, or repeat-volume SMT. |
| AOI | Visible component and solder-joint defects | Repeatable inspection at production speed | Cannot directly inspect hidden joints; program quality matters | For most automated SMT production, with validated coverage. |
| X-ray | Hidden joints and selected internal features | Provides visibility unavailable to ordinary optical inspection | Additional cost; interpretation and acceptance criteria are important | For BGA, QFN, and other relevant hidden-joint risks. |
| ICT | Electrical opens, shorts, and selected component checks | Can provide structured electrical fault detection | Fixture and test-point access may be expensive or restrictive | For stable products with sufficient volume and test access. |
| Functional test | Product-specific behavior and interfaces | Checks whether defined functions operate | Coverage depends on test design; may miss latent defects | When product behavior, interfaces, or operating limits matter. |
For a prototype, a well-designed visual inspection, targeted electrical checks, and functional test may provide an appropriate starting point. For a dense production assembly, AOI plus selected X-ray and electrical tests may be justified. For safety-critical or highly consequential products, the quality plan should be developed with the relevant regulatory, reliability, and engineering requirements in mind rather than copied from a standard consumer-electronics workflow.
5. Benefits and Limitations of PCBA Quality Control
What a strong control plan delivers
Fewer defects reaching customers: Early detection and process correction reduce the chance that known assembly problems move downstream.
More predictable production: Defined setup, inspection, and release criteria make output less dependent on individual judgment.
Faster root-cause analysis: Traceability and defect records help connect failures to a component lot, process step, or production batch.
Lower lifecycle cost: Preventing repeat defects can reduce rework, scrap, returns, warranty claims, and disruption to the OEM's schedule.
Better supplier accountability: Shared acceptance criteria reduce disagreements about whether a board is acceptable.
What quality control cannot guarantee
Inspection and testing reduce risk; they do not eliminate it. A test can miss an intermittent fault, a latent material issue, or a failure that only appears after extended use. Functional testing also cannot compensate for incomplete requirements. If the test does not exercise a critical interface or operating condition, a passing result provides little evidence about that untested behavior.
Quality controls also have a cost. X-ray inspection, custom ICT fixtures, environmental testing, and extensive traceability can increase price and lead time. The right question is not whether to add every available test. It is whether each control addresses a credible failure mode and produces evidence that matters to the OEM.
6. Pros and Cons of a More Rigorous Quality Plan
| Pros | Cons and Trade-Offs |
|---|---|
| Improves defect detection and supports process correction before shipment. | Additional inspection steps can increase manufacturing cost and cycle time. |
| Provides records for supplier reviews, customer audits, and failure investigations. | More data has limited value if the records are incomplete or nobody acts on them. |
| Helps establish consistent acceptance criteria across prototype and production stages. | Test fixtures and inspection programs require engineering effort and maintenance. |
| Can reduce expensive field returns and repeated rework when controls target real risks. | Over-inspection can waste resources on low-risk cosmetic issues while important failure modes remain untested. |
| Supports traceability and controlled handling of nonconforming assemblies. | Traceability requirements may add labeling, scanning, storage, and system-integration work. |
Our position is straightforward: pay for controls that reduce meaningful product risk. Do not pay for a long inspection checklist simply because it looks comprehensive, and do not remove a critical test just to achieve the lowest quotation.
7. Who Needs Which Level of Quality Control?
Prototype teams and startups
For beginners and early-stage hardware teams, the first priority is to validate assembly correctness and product function while preserving the ability to diagnose design issues. Confirm the BOM, inspect placement and soldering, run basic electrical checks, and exercise the main operating modes. If the design uses fine-pitch packages or hidden joints, add targeted inspection rather than assuming visual inspection is enough.
A PCB prototype service is particularly useful when engineering changes are still likely. However, a prototype that passes once is not proof that the design is ready for repeatable mass production. Build a separate pilot-stage plan to validate process repeatability and test coverage.
Established OEMs scaling production
For commercial users, quality control should be standardized across lots and suppliers. Define acceptance criteria, required test coverage, defect reporting, traceability, and escalation rules in the purchase agreement or quality plan. Pilot builds can help reveal assembly and test issues before a production ramp magnifies them.
High-reliability and long-life products
Industrial control, medical, transportation, energy, and other high-consequence applications may require stronger controls, product-specific validation, environmental testing, or formal quality-system evidence. Applicable obligations depend on the end market and product classification. Ask the engineering and compliance teams to define those obligations before choosing inspection levels.
Who may not need every available test?
A low-risk prototype with a short life and simple circuitry may not justify a custom ICT fixture or routine X-ray inspection of every board. A stable, low-density design may not need the same controls as a board with hidden solder joints and expensive field replacement. The correct choice is a documented risk-based plan—not the smallest possible plan and not the largest possible one.
8. Common PCBA Quality-Control Mistakes
Mistake 1: Treating AOI as complete proof of quality
AOI is useful, but it cannot see through a package to verify every hidden solder joint. Combine it with X-ray, electrical testing, or process verification when those methods address meaningful gaps.
Mistake 2: Defining quality as “works when powered on”
A board can power up and still have an incorrect component value, an intermittent connection, a weak solder joint, or a failure in an untested operating mode. Write functional acceptance criteria that reflect actual use.
Mistake 3: Changing components without approval
Substitutions can alter electrical performance, thermal behavior, footprint compatibility, lifecycle, and regulatory status. Require written approval and updated documentation before a substitute enters production.
Mistake 4: Ignoring design-for-test access
If the design has no practical access to important nodes, ICT coverage may be limited or fixtures may become expensive. Consider test points, boundary-scan options, programming access, connectors, and test-mode firmware during design review—not after the board is built.
Mistake 5: Using vague acceptance criteria
Terms such as “good soldering,” “high quality,” or “zero defects” are not enough by themselves. Specify the applicable workmanship standard and class, required tests, sampling rules where used, defect categories, and the procedure for handling nonconforming product.
Mistake 6: Reworking boards without re-verification
Rework can introduce lifted pads, thermal damage, contamination, or new soldering defects. Require suitable re-inspection and re-testing after repair, with records linked to the affected units or batch.
Mistake 7: Choosing a supplier on price alone
A low assembly price can be offset by poor yield, delayed deliveries, weak traceability, and repeated engineering intervention. Evaluate total cost of ownership, including the cost of defects, incoming inspection, and field support.
9. How OEMs Should Evaluate an Assembly Manufacturer
When choosing a PCBA supplier, ask for evidence of the process rather than relying on broad claims about advanced equipment or strict quality control. A capable supplier should be able to explain which checks apply to your board, how the inspection programs are validated, and what happens when a result fails.
Questions to ask before issuing a purchase order
Which revisions of the BOM, assembly drawing, and manufacturing data will be used?
How are component substitutions reviewed and approved?
Which inspection methods are included: visual inspection, SPI, AOI, X-ray, ICT, and functional testing?
What defects can each method detect, and what known gaps remain?
Which workmanship standard and acceptance class will apply?
Can the supplier provide batch-level inspection and test records?
How are failed boards contained, reworked, retested, or scrapped?
What traceability is available for components and finished assemblies?
How are engineering changes communicated and verified on the production line?
What yield, defect, and corrective-action metrics are reported, and how are they defined?
Ask for examples of the actual deliverables you will receive. A sample inspection report, test report, nonconformance report, and revision-control record reveal more than a general statement that the supplier follows industry best practices.
The PCB construction itself also affects assembly planning. An 2-layer PCB and a high-density multilayer board have different layout and inspection considerations. Materials such as FR4 PCB laminates and high-Tg PCB materials must be matched to the thermal and mechanical demands of the design. These substrate choices do not replace assembly controls, but they can affect the process window and reliability risks that the supplier needs to understand.
10. Cost-Benefit Analysis: Where Should You Invest?
There is no universal percentage of the assembly budget that should go to inspection. The economics depend on board value, production volume, defect probability, field-repair cost, test coverage, and the consequences of failure. OEMs should prioritize controls that prevent or detect expensive failure modes early.
| Investment | Cost Driver | Potential Value | Practical Priority |
|---|---|---|---|
| Design and BOM review | Engineering time before release | Prevents avoidable revision, footprint, and component errors | High for nearly every project |
| SPI and AOI | Equipment, programming, line time | Detects many printing, placement, and visible soldering defects early | High for automated SMT, especially complex builds |
| X-ray inspection | Inspection time and equipment cost | Provides evidence for selected hidden-joint risks | Risk-based; especially relevant to hidden terminations |
| Custom ICT fixture | Fixture design and maintenance | Repeatable electrical checks at production scale | Often more attractive for stable, recurring volumes |
| Functional test development | Test hardware, software, engineering time | Verifies defined product behaviors and interfaces | High when functional failures are costly |
| Traceability and reporting | Data capture, labeling, storage, integration | Speeds containment and root-cause investigation | Increase with risk, product lifetime, and customer requirements |
To compare options, estimate the expected cost of defects: probability of failure multiplied by the likely cost of rework, scrap, returns, warranty handling, and disruption. Compare that estimate with the incremental cost of the proposed control. The numbers will be uncertain, but even a rough, documented model is better than choosing tests by habit.
For a low-volume prototype, engineering review and targeted testing may provide more value than an expensive fixture. For stable high-volume production, a fixture can become economical because its development cost is spread across many units. For a safety-critical product, the cost of failure may dominate the calculation, making more rigorous verification justified even at lower volume.
11. Can Fast PCB Assembly Maintain Quality?
Yes—fast-turn assembly can maintain quality when the schedule is supported by a controlled process, complete documentation, material availability, and an inspection plan appropriate to the design. Speed itself is not a quality method, however. A short lead time does not prove that a board has been adequately inspected or tested.
365PCB offers Fast PCB Assembly services for rapid prototyping and quick-turn production, with advertised assembly turnaround as short as 24 to 48 hours for qualifying projects. Actual timing depends on board complexity, component availability, engineering readiness, order scope, and the tests required. OEMs should confirm the schedule and included quality checks for their specific build rather than assuming every order follows the same turnaround.
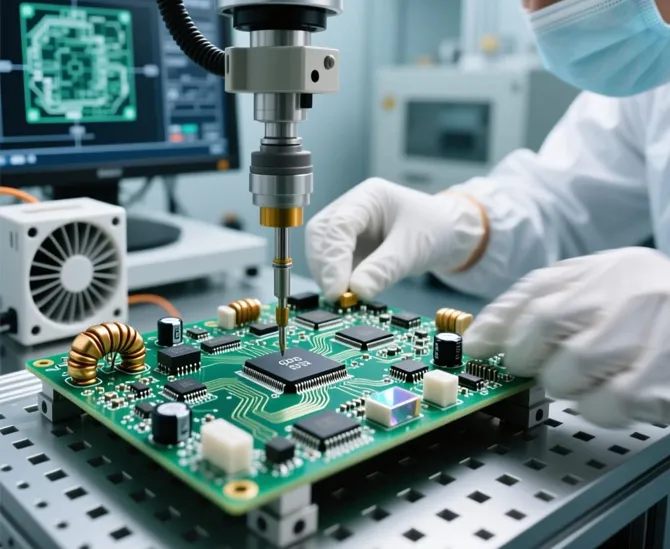
For urgent orders, the best way to protect quality is to remove avoidable delays before the clock starts. Supply a complete and consistent data package, identify approved alternates, clarify acceptance criteria, and specify whether AOI, X-ray, ICT, or functional testing is required. Agree on the handling of failed units and whether inspection records must be delivered with the batch.
We recommend asking a quick-turn supplier three direct questions: What quality checks are included in the quoted lead time? Which checks require additional time or cost? What evidence will be available before shipment? Clear answers make it easier to balance speed, cost, and risk.
12. Expert Recommendation: Build Quality into the Order
Our recommendation is to treat PCBA quality control as a joint engineering and sourcing decision, not a final inspection add-on. The OEM knows the consequences of product failure; the assembly manufacturer understands the manufacturing process. Both sides should agree on how those risks will be controlled before production begins.
Classify the product risk. Consider safety, operating environment, service life, repairability, and the commercial impact of a failed unit.
Release one controlled data package. Align the BOM, drawings, fabrication data, placement files, approved alternates, and test requirements.
Choose tests by failure mode. Use AOI for visible defects, X-ray for relevant hidden-joint risks, ICT for suitable electrical coverage, and functional testing for defined product behavior.
Define acceptance and escalation. Document workmanship criteria, sampling rules, rework approval, retesting, traceability, and shipment release.
Review the first build before scaling. Evaluate yield, recurring defects, test coverage, and corrective actions before committing to larger volumes.
Track results across production lots. Trend defects and yield, investigate repeat issues, and verify that corrective actions remain effective.
For OEMs working on dense, specialized, or mechanically demanding boards, early collaboration is particularly valuable. For example, a bendable PCB may require handling and strain controls that would not be relevant to a rigid board, while a laser-drilled PCB may have design and fabrication considerations that affect the overall engineering review. Match the assembly quality plan to the real product rather than using a generic checklist for every order.
The best supplier is not necessarily the one offering the most inspection steps. It is the one that can explain the risks, demonstrate the controls, provide meaningful records, and respond effectively when results do not meet requirements. That is the standard OEMs should use to judge PCBA quality control.
13. Frequently Asked Questions
What is PCBA quality control?
PCBA quality control is the set of inspections, electrical tests, process checks, material controls, and documentation used to verify that an assembled circuit board meets its specified requirements. It covers the manufacturing process as well as the finished assembly.
What is the difference between PCB quality control and PCBA quality control?
PCB quality control focuses on the bare printed circuit board, including its materials, dimensions, copper features, holes, and electrical integrity. PCBA quality control covers the populated board, including component identity and placement, solder joints, assembly workmanship, electrical behavior, and product-specific tests. OEMs often need both, because a correctly assembled board can still be affected by a defect in the bare PCB.
Is AOI enough for PCBA quality control?
No. AOI is effective for many visible component and soldering defects, but it cannot directly inspect hidden solder joints or prove full electrical functionality. Depending on the design, a quality plan may also need SPI, X-ray, ICT, functional testing, and process controls.
When should an OEM require X-ray inspection?
X-ray is worth considering when the assembly contains hidden solder joints, such as those under certain BGA or QFN packages, and when those joints represent a meaningful risk. The inspection criteria should be appropriate to the package and product requirements. X-ray should not be treated as a universal substitute for electrical testing or process validation.
Does every PCBA order need ICT?
No. ICT can be valuable for stable designs and repeat production when suitable test access is available, but fixture development may not be economical for a small prototype or a frequently changing design. In those cases, targeted electrical checks and a well-designed functional test may be more practical.
Which quality standards should OEMs specify?
Specify standards that apply to the product and market. IPC-A-610 is commonly used for electronic assembly acceptability, while J-STD-001 addresses requirements for soldered electrical and electronic assemblies. The applicable revision, class, and contractual requirements should be agreed explicitly. A standard reference alone does not replace a product-specific test plan.
Can fast PCB assembly meet OEM quality requirements?
Yes, provided the supplier has the required materials, complete engineering data, suitable process controls, and enough time to perform the agreed inspections and tests. Confirm the included checks and release documentation before approving a quick-turn schedule.
What should be included in a PCBA quality report?
Depending on the project, the report may include lot or serial identification, inspection results, test coverage and outcomes, defect summaries, rework and retest records, nonconformance disposition, and shipment-release status. Define the required format and retention period before production.
How can OEMs reduce PCBA defects without increasing costs unnecessarily?
Start with document and BOM accuracy, review manufacturability and test access, target inspection at high-risk failure modes, and track repeat defects. Add specialized inspection or fixtures when their expected risk reduction justifies the cost. Avoid paying for checks that do not provide useful coverage while leaving critical failure modes unaddressed.
14. References
The following authoritative sources provide background for workmanship acceptance, soldered assembly process requirements, and electronics quality-system practices. Confirm the current edition and applicability before incorporating a standard into a contract.
IPC — Standards for electronics manufacturing and assembly. Consult the applicable IPC-A-610 and J-STD-001 documents for assembly acceptability and soldered assembly requirements.
International Organization for Standardization — ISO 9001:2015, Quality management systems. Provides a framework for controlled processes, documented information, and continual improvement. Verify the current edition and any amendments on the ISO website.
National Institute of Standards and Technology — Information Technology Laboratory. Offers technical resources related to measurement, testing, and standards-based engineering practices.
Note: Acceptance criteria, inspection coverage, sampling plans, and regulatory obligations should be tailored to the product, contract, and target market. No single inspection method guarantees defect-free performance.